Case file 03 · RV OEM
RV OEM Cut-Out Consistency: No Line Changes, No Dimensional Drift
A component family was locked to a recess the vehicle already used, and one out-of-spec batch could stop the station behind it. The record below is what it took to make every lot line-ready.
- 100%
- Lots released inside the frozen tolerance
- 50,000+
- Components against the frozen revision
- 22 lots
- Released on the final gate, none held
- $250k est.
- Stoppage and retooling cost prevented
Client profile
Who the Cut-Out Program Was Built For
An anonymised Tier-1 / Tier-2 RV OEM building one critical component family to a recess its existing line already used.
- Program
- One critical component family inside an RV OEM
- Constraint
- Locked recess, existing line stations, existing operator sequence
- Control basis
- One frozen drawing revision, ballooned for inspection
- Per lot
- Variable-data measurement against the locked revision
- Tooling
- Dies, jigs, fixtures and routing templates, logged by hit count
- Forcing function
- Line throughput and service-parts continuity after launch
- Client name
- Withheld under NDA
Company profile linked for reference; the program figures are anonymised.
Summary
What Held the Cut-Out Steady
This is one critical component family inside an anonymised Tier-1 / Tier-2 RV OEM program, not a claim about every RV model or model year. Fitment had to be exact: a batch that measured close on paper still needed a shim on the line.
Gulfstone locked the released revision, converted the fit-critical features into a measured control plan, and audited tooling life during the run. 50,000+ components shipped against that frozen record.
Every lot inside the approved report window passed the final dimensional gate against the locked revision, and the OEM plant made no line changes for the covered program. The eight-step path behind both is set out below.
The $250,000 in prevented stoppage and retooling cost is an estimate. It is priced against the shim and fixture-edit rate the program replaced, not against a single documented invoice.
- 100% — Lots inside the frozen tolerance
- 50,000+ — Components delivered against the frozen revision
- 22 lots — Released on the final gate, none held
- $250k est. — Prevented stoppage and retooling cost
- Skip it — For one-off prototypes or a program still changing its drawing
The RV Industry Association tracks North American RV production, and the launch cadence behind it raises the cost of every dimensional surprise.
I
Why Does Dimensional Drift Stop an RV Line?
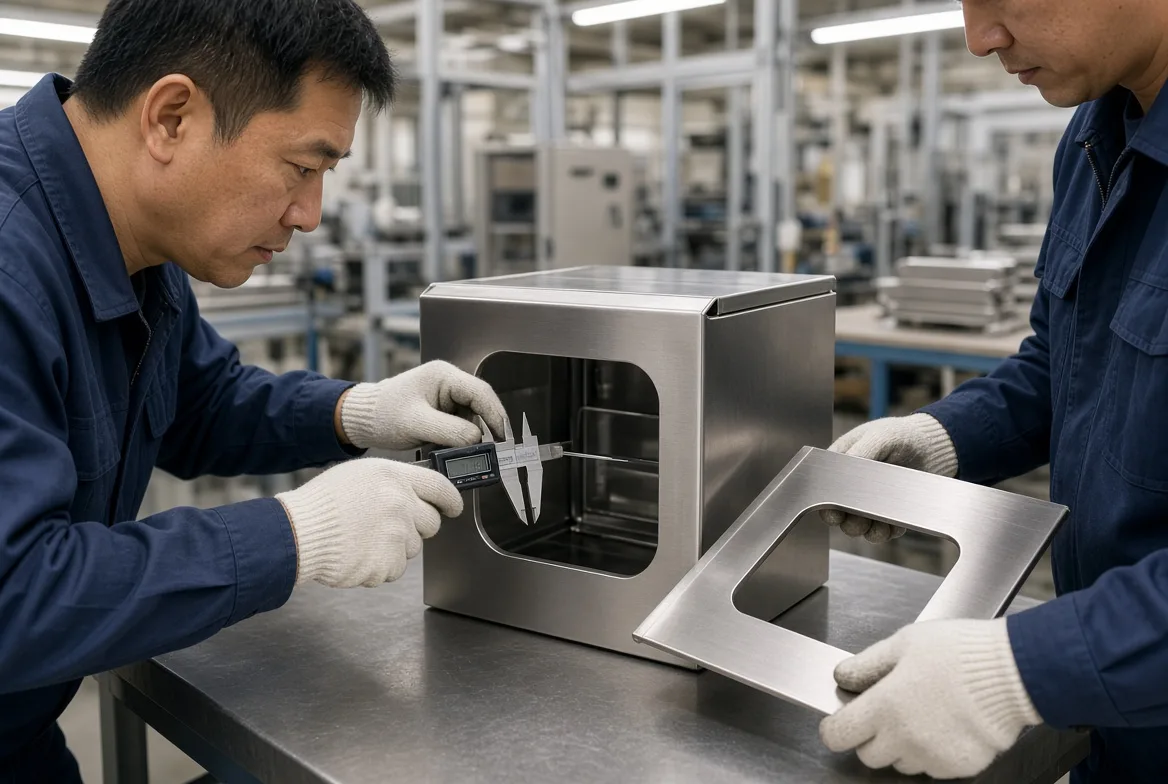
A water heater cut-out is a stack of tolerances — framed opening, brackets, gasket face and trim line. A part can pass the drawing and still fail the station, and the line pays the difference.
Plant leadership protected takt time above all. One out-of-spec batch breaks station balance, forces line-side improvisation and weakens receiving confidence in every later shipment. One bad batch became a three-day ripple.
The pain was the stack. A part could measure close on paper and still fail on the line. If the bay had to trim foam, enlarge an opening or change clamp pressure to make it fit, the part was not usable.
The cost arrived fast: line slowdowns, emergency fixture adjustment, added labour for trim and reseal, later leak and corrosion risk, and procurement distrust once approved parts stopped behaving like approved parts.
The cause was never single. Material movement, supplier process drift, undocumented program edits and tooling wear compounded over time. A fix aimed at one factor failed within weeks.
“The part was within spec, but it was not line-ready.”
What Drift Costs a Locked Line
- Line stoppage and slowdown. One out-of-spec batch breaks station balance, and the ripple reaches the schedule within a day.
- Emergency fixture adjustment. Maintenance work nobody planned, on a line that then runs on a modified fixture until the next change.
- Trim, shim and reseal labour. Labour the standard time never carried, repeated on every batch until someone finds the cause.
- Service-parts mismatch. A replacement that no longer drops into the cut-out made from the same drawing.
The Batch That Passed CMM and Still Needed a Shim
The batch passed the CMM inspection report against the approved drawing.
The same parts still needed a 2 mm shim to sit at the station. Paper tolerance and line reality had parted company.
Within spec stopped counting as the finish line. Pass/fail data alone could not show where the geometry was trending.
The Rules That Govern a Fitment Program
- A drawing tolerance is a band; station fit is a point. The narrower of the two decides whether the batch ships.
- Go/no-go gauges accept the part in front of them and say nothing about the trend behind them.
- Tooling wears quietly: hit counts, edge wear, fixture fatigue and thermal distortion move geometry while the paperwork still reads clean.
Ask the supplier for a ballooned drawing and variable measurement against it, per lot rather than per sample. A pass/fail report cannot show drift; a trend line can.
II
What Is Cut-Out Dimensional Control?
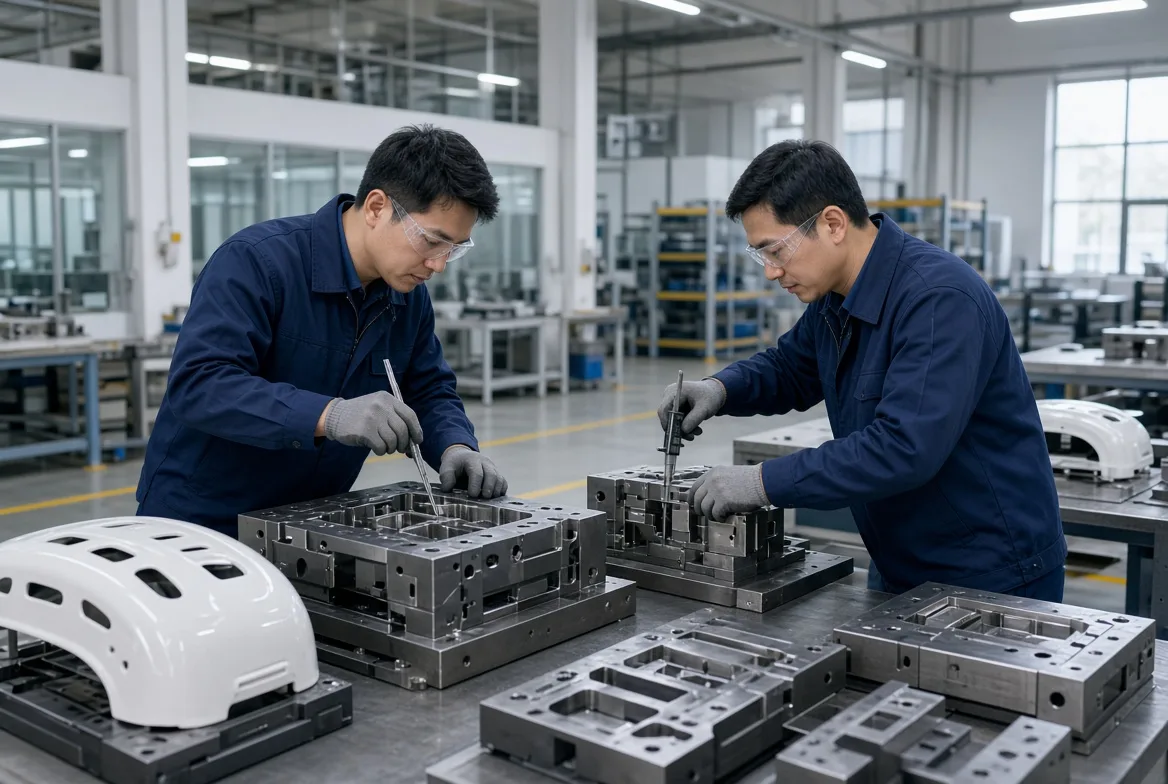
It is a release discipline: one frozen revision, every fit-critical feature turned into a measured gate, tooling life audited during the run, and no container released until the lot matches the record.
A PPAP-style dimensional report records measured results against the approved drawing. It is one artifact in the control stack, not the stack itself, and on its own it does not guarantee drop-in fitment.
What held this program was the path around the report: the drawing freeze, the converted control plan, the tooling audit and the final lot gate. Each exists because drift is cheaper to prevent than to detect.
The Four Gates Before the Booking
Revision · Is There One Master Record?
The released CAD, drawing revision and cut-out-critical dimensions are frozen. Engineering change notices control every move; no CNC edit, material substitution or tooling tweak advances without sign-off.
Control plan · Does Every Fit Feature Have a Gate?
The drawing is ballooned into a PPAP-style checklist: nominal dimensions, tolerance bands, mating surfaces, hole locations, flange depth and sealing interfaces, each with a gauge method and a sample size.
Tooling · Is the Tool Validated Before the Run?
Dies, jigs, routing templates and fixtures are reviewed against master samples before the first cut. Approved tooling still degrades, so hit counts and cutting edges are logged from day one.
Release · Does the Lot Match the Locked Record?
The final dimensional gate compares the lot to the frozen revision and its sampling plan. Nothing loads until it passes, and the receiving lead signs the release.
When the Part Still Moves, Three Answers Decide
Return to tooling
Geometry drifting inside the run: stop, service the die and re-qualify with variable data before restarting.
Raise an ECN
A deliberate design change becomes a new revision and a repeated first article, never a silent program edit.
Hold the lot
An out-of-spec measurement holds the lot until the record and the part agree again.
The Measurements Behind the Gate
- First article
- Micrometer, caliper, dedicated go/no-go gauges and variable measurements, with CMM or laser-scan spot checks where geometry is complex.
- Variable data
- A continuous measurement shows where a batch is trending. Go/no-go gives pass or fail and hides the trend.
- Tooling life
- Hit counts per die, cutting-edge inspection on a fixed schedule, fixture wear and thermal distortion.
- Sampling plan
- Sample size per feature, set by part family, material and volume. High-volume, abrasive or thermal-sensitive parts get tighter checks.
- Release record
- Lot number matched to the locked revision, final gate results and receiving sign-off, filed per shipment.
The gates are the same on any fitment program. The tolerance band and the sample size are what change.
“Pass/fail says whether the part in front of you is acceptable. It says nothing about the one you will make next week. Variable data on a trend is what holds a cut-out across 50,000 parts.”
III
The Control Path From Drawing Freeze to Container Release
The steps run in sequence, and each one closes a door that drift would otherwise come through.
Freeze the Engineering RecordFreeze
The released CAD, drawing revision and cut-out-critical dimensions are locked before production. Engineering change notices control every move: no CNC program edit, material substitution or tooling tweak advances without sign-off. The approved revision becomes the only master record.
Convert the Drawing Into a Control PlanPlan
The drawing is ballooned into a PPAP-style checklist covering nominal dimensions, tolerance bands, mating surfaces, hole locations, flange depth and sealing interfaces. Each feature carries a tolerance band, a gauge method and a sample size.
Validate Tooling Before the RunTool
Dies, jigs, routing templates, fixtures and master samples are reviewed before the first cut. Hit counts, edge wear, router-bit wear, thermal distortion and fixture fatigue are tracked from day one, with cutting edges inspected on a fixed schedule.
Run First-Article Verification at OriginFAI
The first article goes through micrometer checks, caliper checks, dedicated go/no-go gauges and variable measurements. For complex geometry the team adds CMM or laser-scan spot checks, because go/no-go alone cannot show a trend.
Approve Through a PPAP-Style PacketPPAP
The submission includes ballooned drawings, measured sample data, gauge results, a master-sample comparison and sign-off records. The packet supports approval; it does not replace line-fit validation.
Audit In-Process Stability, Not Just StartupMonitor
Tooling-life audits run through production, so cut-out drift is caught before shipment. Startup quality is a snapshot; in-process stability is the control that keeps the batch line-ready.
Control Environment and PackingStore
Climate-sensitive substrates and stored panels can move after machining. Dimensional fidelity depends on storage, stabilization, packing and protection, so parts stay flat, dry and supported before loading.
Release Only After Final Lot VerificationRelease
No container loads until the lot clears the final dimensional gate. Lot records must match the approved revision and sampling plan, and the receiving lead signs the release before the container is sealed.
The Standard Path, and the Exceptions That Stop a Lot
The standard path runs from drawing freeze to sealed container. The exception path handles the four moments when a lot must stop moving.
Standard pathFreeze to release
Lock CAD, revision and fit-critical dimensions
Number every feature; assign gauge and sample size
Measure variable data; compare to the master sample
Audit hit counts, edge wear and trend lines
Match the lot to the locked revision; sign release
Exception pathWhen a lot stops
Outside the plan: service the die and re-qualify before restart
An ECN and a new revision, never a silent program edit
The lot is held while the record and the measurement disagree
Re-measure climate-sensitive parts after storage, before loading
IV
The Quality Engineer on Where Geometry Moves
Chen leads quality and sourcing at Gulfstone and owned the release conditions on this program: the revision freeze, the tooling-life audit and the final lot gate.
Chen
Lead Quality and Sourcing Engineer, Gulfstone
What hidden issue drives tooling degradation overseas?
Suppliers often track output, not tool life. A die or router bit keeps cutting after wear starts, so geometry moves while the paperwork still looks clean.
What signals do you watch before parts go visibly out of spec?
We watch hit counts, edge wear, fixture wear and small shifts in variable data. A trend line matters more than one acceptable part.
How does audit frequency change?
Part family, material and volume set the cadence. High-volume, abrasive or thermal-sensitive parts get tighter checks.
In this program the in-process audit caught cut-out drift before shipment. A trend in variable data stops a lot from loading; a failed gauge only stops it after the drift has already travelled.
V
RV OEM Cut-Out Results: A Frozen Record, Held at the Gate
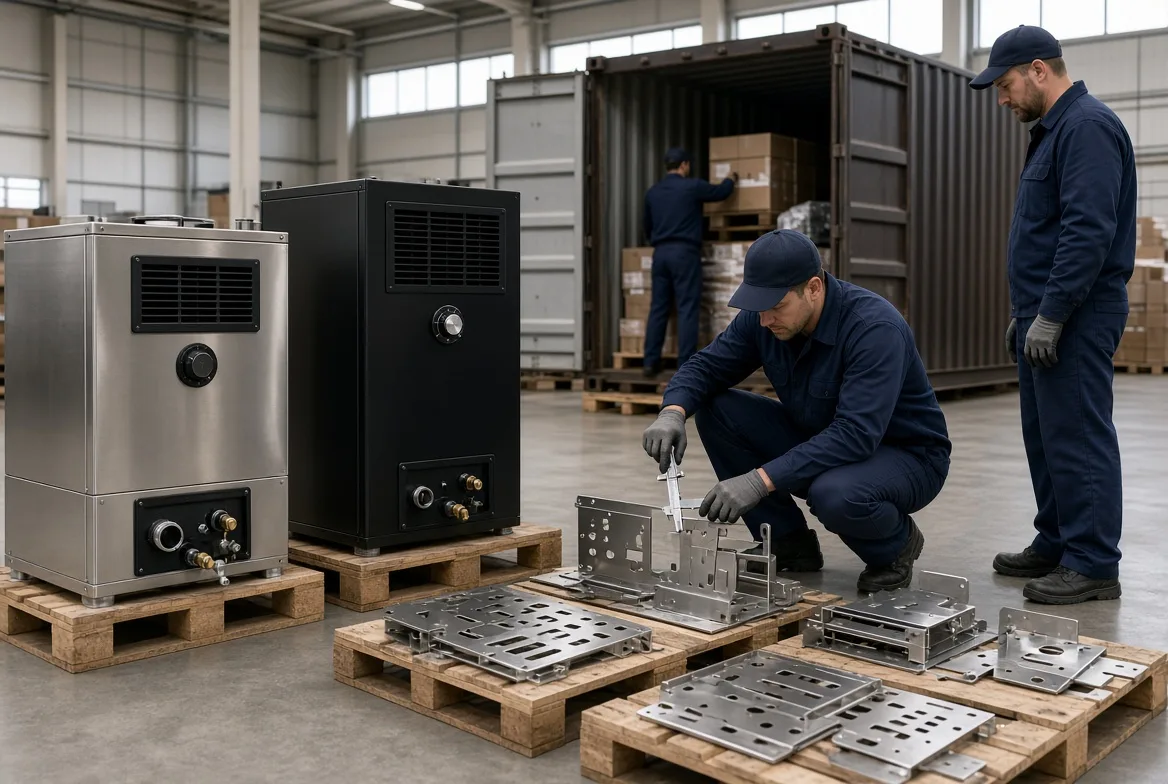
One anonymised component program, measured across shipment and inspection records. The 100% covers the approved report window only; it is not a whole-history claim.
| Measure | Program record | Basis |
|---|---|---|
| Components delivered | 50,000+ | Against the frozen drawing revision |
| Lots inside tolerance | 100% | Approved report window |
| First-article approval | Approved on the first submission | Against the locked revision |
| Station shims | 0 | Every lot released on the final gate |
| Service replacement | Drops into the original cut-out | Same drawing, same revision |
| Stoppage and retooling | ~$250,000 avoided | Estimate, priced on program volume |
How the Record Was Held
Drawing control
Moving
Revision edits reached the line without a record behind them
Drawing control
Frozen
One master record, with an ECN for every change
Lot acceptance
100%
Released against the locked revision, approved report window
The $250,000 is an estimate priced against the program volume and the industry downtime-cost reporting. The pre-program stoppage cost itself was never invoiced as one line, which is why the figure is stated as avoided cost rather than a measured delta.
Each lot number was matched to the locked revision, and the final gates were read at origin. The 100% covers the approved report window only. The cost outcome is an estimate priced from the pre-program shim and fixture-edit rate, not a measured delta.
Gulfstone ran the program and its internal quality team gathered the data. No supplier, testing body or carrier paid for this case study, and the client's name is removed.
- Station sequence unchanged: no line rebalance, no fixture edit, no operator resequencing.
- Receiving friction down: fewer walk-backs from receiving to engineering on approved parts.
- Trim and shim labour gone from the standard time on the affected station.
- Service-parts continuity: a replacement drops into the cut-out cut from the same drawing.
“The line never asked us for a shim. Tooling held geometry, so nobody improvised.”
VI
What Transfers From a Cut-Out Program
Four controls carried the result. Each is cheap before the run and expensive after it.
Define fit-critical dimensions before quoting
A ballooned drawing returned with the quote shows what the supplier thinks it is making. A generic within-tolerance assurance shows nothing.
Require production-part approval, variable data and tooling-life audits
Pass/fail gauges hide drift. Make the logs a release condition, not a monthly report nobody reads.
Control storage and packing after machining
Climate-sensitive parts move after they are cut. Flat, dry and supported storage is part of the tolerance, not a warehouse detail.
Protect lifecycle support from day one
Revision IDs and lot traceability are what let a replacement drop into a cut-out made two years earlier.
Require each supplier to return the drawing with every fit-critical feature numbered, toleranced and assigned a gauge method. That document becomes the quote basis and the inspection basis at once.
VII
Why the Cut-Out Discipline Scales
RV makers face faster launches, leaner staffing and more variants. Every added configuration multiplies the cut-outs a line has to accept, and raises the cost of each dimensional surprise.
The program held because the control sat at origin, before the container. The next step for a buyer is not another supplier search; it is a drawing review that names the fit-critical features and the trend that proves them.
Frequently Asked Questions About RV Cut-Out Consistency
1. How do you keep RV cut-outs from drifting out of tolerance?
Freeze the released drawing revision, turn cut-out-critical features into a measured control plan, and audit tooling life during the run. Here the team tracked hit counts, edge wear and variable data, so drift showed on the record before a part failed. Final lot verification blocked shipment until each lot matched the revision.
2. What is a PPAP dimensional inspection report?
A PPAP dimensional inspection report records measured results against the approved drawing, and it does not by itself guarantee drop-in fitment. PPAP means Production Part Approval Process. Here the report sat inside a longer stack: ballooned drawings, sample data, gauge results and sign-off records. Approval still did not replace line-fit validation.
3. Do go/no-go gauges work for RV parts?
Go/no-go gauges work for fast pass/fail acceptance on RV parts, but they cannot show drift before a part fails. In this program the team used go/no-go checks plus variable measurements, with CMM or laser-scan spot checks for complex geometry. That combination made tooling wear and trend lines visible, which go/no-go alone cannot do.
4. Why does a replacement part no longer fit an RV cut-out?
A replacement that no longer fits usually means the revision moved without a record: a silent program edit, tooling wear or a supplier change between lots. In this program every lot was matched to the locked revision before release, so a service replacement drops into the cut-out made from the same drawing.
Forward
Co-founder & General Manager, GulfstoneGas appliance manufacturing and certification
Most of what decides a gas appliance is settled before anything is built — on the drawing, at the cut-out, in the tolerance someone chose for the gas path. I have spent my working life on the manufacturing side of that decision, and this is where I write down what it has taught me.
Nothing here is written from a sales desk. Every note comes off the floor: a batch held until a reason was found, a fitting that failed in transit, an approval path that only made sense once the destination market was fixed. If you read these first, the opening conversation starts at the standard rather than at the beginning.
- Gas water heater engineering
- Design for manufacturing
- Certification path selection
- Private-label tooling
- Off-grid and outdoor water heating
- Top 8 Outdoor Portable Gas Water Heater Factories in China for B2B BuyersNov 4, 2026
- Custom RV Appliance Industrial Design: An OEM Brief to a Validated PrototypeNov 3, 2026
- How to Build Custom Thermostat UI Design Software for OEM Embedded PanelsNov 3, 2026
- Top 8 RV Water Heater OEM Suppliers Canada: Vetted for Volume BuyersNov 3, 2026
Fifteen years in appliance manufacturing — home appliances, RV refrigeration, then gas water heating — from the drawing to the shipping container.
Leads Gulfstone's design-for-manufacturing reviews and the certification path selected for each destination market.
Works directly with OEM and private-label buyers on tooling, tolerances and the approval file.