Table of contents
The Short Answer
- A gas appliance testing laboratory proves a unit holds pressure, burns safely, and meets the standard of the market you sell into.
- Testing, calibration, accreditation and certification are four different things, and only an accredited body issues the approval that clears your shipment.
- A room of instruments proves nothing without current calibration, retained records and operator competence.
- Pressure-decay testing is only as good as the fixture — a creeping valve on the rig mimics a leaking product.
- Budget in-house screening, third-party testing, and certificate maintenance as three separate lines, because a factory lab never erases the third-party bill.
A gas appliance testing laboratory is the in-house facility where a factory proves, under its own roof, that a unit holds pressure, burns safely and meets the certification standard of the market you sell into.
We have spent years on the floor in Guangdong, and we have watched units pass cosmetic QC and then fail at a notified body in Europe or a lab in North America. They leaked. Their pressure control drifted. Their combustion data never matched the paperwork. The factory lost the order, and the buyer lost the spring window.
This briefing is for QA directors, supply-chain leaders and chief engineers who have to decide whether a factory’s bench is credible enough to trust before approving mass production. Export-market risk lives here. A clean sample means nothing if the lab that tested it runs uncalibrated gauges and skips records.
It rests on witnessed bench practice, export certification pathways, and the supplier audit checklist our team carries on the floor. What follows is documented procedure and witnessed test, not supplier marketing.
What Is a Gas Appliance Testing Laboratory?
Gas safety testing for appliances is the controlled verification of how a gas product behaves under pressure, heat and fault. A gas appliance testing laboratory is the room where that work happens — a controlled environment where gas products, assemblies and safety-critical components are checked for leak-tightness, pressure behaviour, combustion stability, emissions and safety-device response.
Four terms get blurred together, and we separate them on every bench review:
- Testing runs a product through a defined procedure and records the result.
- Calibration proves an instrument still reads true against a traceable reference.
- Accreditation is formal recognition, under ISO/IEC 17025, that a laboratory is competent to run a defined scope of tests.
- Certification is the final market approval, issued only by a body with the legal authority to grant it.
A factory lab can run pre-compliance testing all day long. That does not make it the certificate issuer. Only an accredited third party or a notified body signs the approval that clears your shipment.
Lab type matters in the same way. An in-house OEM lab tests the factory’s own production line. A witnessed setup lets your engineer stand at the bench and watch the run. An external third-party body carries accreditation and issues reports you can defend at customs.
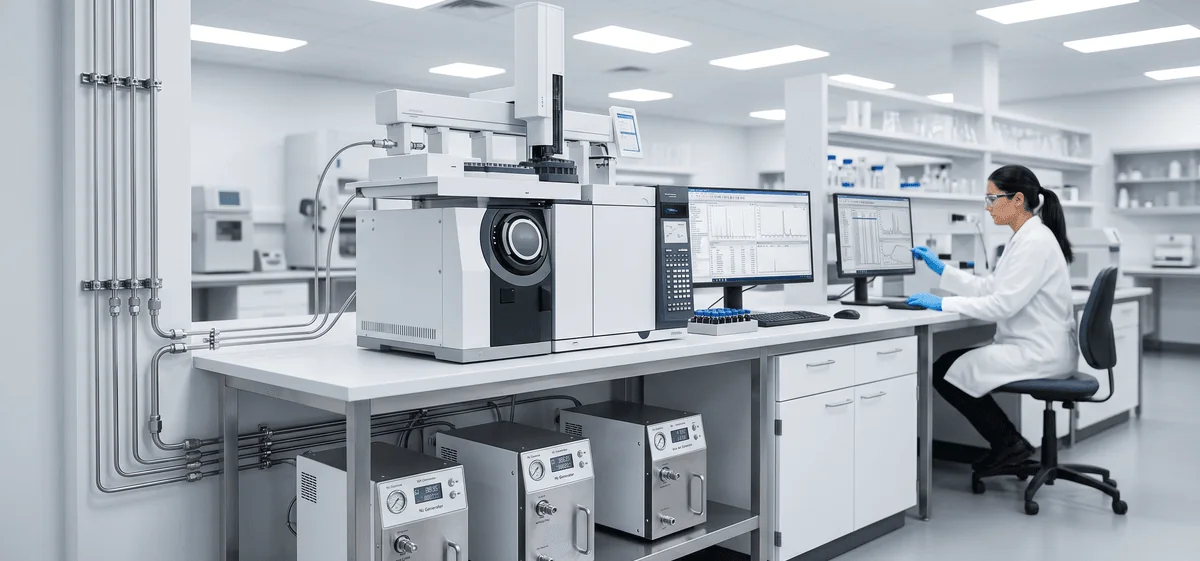
Expect this baseline equipment: calibrated pressure gauges, flowmeters, leak detectors, temperature measurement, timed test controls, gas supply regulation and combustion analysis capability. On a Foshan line we reviewed last quarter, the bench gauge was eight months past its calibration date. Soundness testing, flame-failure protection and emission checks mean nothing if the instruments lie.
💡 Diagnostic Tip: Ask the lab for its instrument status sheet before you ask for any test report. An uncalibrated gauge invalidates every reading taken after it, however clean the report looks.
Which Standard Applies, by Market
The standard follows the appliance family and the destination market — not the factory. Getting this wrong is the most expensive mistake a program can make, because the retest lands after tooling.
- Europe: Regulation (EU) 2016/426, the Gas Appliances Regulation. Product standards run per family — EN 30-1-1 for domestic cooking appliances, EN 26 for instantaneous water heaters, EN 89 for storage water heaters, EN 203-1 for catering equipment. Control components are covered by EN 298, EN 161 and EN 13611, tested on the test gases and test pressures defined in EN 437.
- North America: the ANSI Z21 / CSA 2.x series. ANSI Z21.10.1/CSA 4.1 and Z21.10.3/CSA 4.3 for water heaters, Z21.47/CSA 2.3 for central furnaces, Z21.58/CSA 1.6 for outdoor cooking appliances, Z21.86/CSA 2.32 for vented space heating. Field-approval work runs to CSA B149.1 and B149.3.
- China: GB 16410 for domestic gas cooking appliances, GB 6932 for instantaneous water heaters, GB 25034 for gas-fired heating boilers. GB 16914 sets the general safety conditions and GB/T 16411 the general test methods.
The same heater can face a different standard, a different test gas and a different evidence trail in each market. Our own quality system is built around that split, and the destination standard is fixed before a drawing is released.
🧠 Expert Take: A room of instruments proves nothing on its own. Match scope, calibration status, records and operator competence to the exact products you are auditing. Otherwise you are paying for scenery.
How Testing and Certification Work Inside the Factory Lab
Gas appliance testing and certification runs in two linked stages: the factory lab proves the unit before submission, and an accredited body issues the approval that clears your shipment. For OEM gas heaters and outdoor water heaters, the separator is not whether a factory says it has a lab. It is whether that lab can reproduce the failure modes that later cause CSA or CE setbacks.
We trace this workflow step by step on our own bench. Everything below covers pre-submission verification, and none of it replaces the final certification decision.
Fixture setup and calibration check
Purpose: a trustworthy baseline. Before anyone energizes the bench, we verify gauge class against the test range, leak detector readiness, gas source stability, ambient conditions, timer function and sample identification. The instrument carries a current calibration record, or the bench stays off.
Records: instrument status sheet, ambient log, sample ID tag.
Leak detection screening
Purpose: find leaks before they confuse pressure readings. We scan joints, valves, manifolds, burners, fittings and threaded connections with soap solution or a detector-led method. Micro-leaks hide at threaded connections and manifold caps. Any hit goes to rework, not to pressure testing.
Records: joint-by-joint leak checklist.
Pressure-decay verification
Purpose: confirm the assembly holds gas over time. The operator fills the assembly, allows stabilization, holds for a timed interval, then reads pressure loss. Pass or fail depends on stable fixtures and calibrated instruments, never on a glance at the dial.
Records: fill pressure, hold time, loss reading, operator signoff.
Combustion and emissions testing
Purpose: confirm clean, stable combustion. We check ignition stability, flame shape, flame-failure response, heat input and combustion values under the target gas family and operating condition. Two points matter more than they look.
The governing metric is the CO/CO₂ ratio, not raw CO in parts per million. The ratio normalises for dilution and excess air, which is why every combustion criterion is written around it — a raw ppm figure taken on the wrong analyser setup sends teams chasing a problem that is not there.
The applied test gas and test pressure come from EN 437 in Europe, or the equivalent national schedule elsewhere. A portable outdoor water heater on LPG behaves nothing like the same unit on natural gas.
Records: analyser output, gas family, operating condition.
Pre-certification review and traceability release
Purpose: confirm the sample matches the design. We check the report pack against sample identity, the bill of materials and design drawings. The operator signs. Only then do we mark which samples proceed to third-party or formal certification submission.
Records: the complete test pack.
Failure modes do not wait for a tidy sequence, so we log each one as symptom, root cause, corrective action and re-test checkpoint.
| Symptom | Root cause | Corrective action | Re-test |
|---|---|---|---|
| Yellow flame tips, CO spikes | Unstable primary-air ratio | Reset the air shutter, confirm injector size | Full and part load |
| Flame rollback or lift | Burner-port burrs, injector mismatch | Deburr the ports, fit the specified injector | Ignition and flame shape |
| Slow manifold decay | Manifold sealing failure | Reseat or replace the gasket | Repeat the timed hold |
| Flame signal dropping mid-run | Flame-sensing misalignment, valve regulation drift | Realign the sensor, verify valve regulation | Flame-failure simulation |
| CO rising outdoors only | Wind-shielding and venting effects | Adjust shroud geometry | Shielded and unshielded runs |
RV gas appliances surface these faster than portable units. The chassis envelope restricts airflow, so venting faults show up early — the same enclosure behaviour our RV engineering work runs into when a burner is asked to hold a flame in a moving airstream.
🌍 Real-World Context: A creeping valve on the test rig looks exactly like a leaking product. We prove the fixture holds before we blame the unit, because the alternative is reworking good assemblies.
Q&A: what fails first, and what the bench can fix
Q1: What combustion failures show up most on the first run?
Chen: Ignition instability and CO spikes. They usually trace back to air ratio or a fouled burner port.
Q2: Which failures come from design geometry rather than assembly drift?
Chen: Wind-shielding and venting are geometry problems. Valve regulation drift and flame-sensing misalignment are assembly drift.
Q3: Which can be fixed before certification sampling, and which need redesign?
Chen: Injector mismatch, burrs, sealing and sensor alignment we fix on the bench. Venting geometry that fails under wind load usually needs a redesign.
Q4: What paperwork mistake most often invalidates a good test?
Chen: A sample ID that does not match the bill of materials or the drawing revision. The test itself was fine. The traceability was not.
Hand-off to external approval
The in-house workflow exists to reduce surprises, not to replace anyone. Once the pack is signed, samples move to a notified body or an approved body for formal acceptance. In Europe or Great Britain that is a body such as BSI (notified body 0086) or Intertek (approved body 0359); in North America, a certification body for the relevant ANSI/CSA standard.
Expect the reviewer to ask for access to the type-examination report, the design documentation, the production line and the facilities. Surveillance runs at least annually, and can be reduced in scope if your quality system is accepted. Serial production must remain identical to the approved type. Our bench proves readiness; it never issues the certificate. The documents that travel with a shipment are the ones catalogued on our certifications page.
Benefits of an Integrated Factory Bench
An integrated factory bench pays off when it shortens feedback loops, catches first-run failures earlier, and lowers the odds that bad units advance to expensive certification or field exposure. The advantage is rarely the equipment itself. It is the shorter corrective-action cycle that records, calibrated tools and repeatable procedures make possible.
Faster engineering correction
An integrated bench surfaces root causes before external lab scheduling and sample shipping. We run leak, pressure-decay, combustion and safety-device checks on one bench, under one quality system. That upstream control catches injector mismatches, seal defects and sensor drift while the fix is still cheap. A manifold gasket reseat took one bench cycle, not a four-week external retest. Engineers fix the design before the sample leaves.
Lower recall exposure
Leakage, combustion and safety-device failures get removed earlier in the product lifecycle. The goal is fewer failures reaching certification, customs or the field — not zero failures on the bench.
EU Gas Appliances Regulation pathways and CSA/ANSI-facing expectations reward evidence of pre-submission control. The Chinese implementation-rule mindset around traceability and inspection discipline reinforces the same point: catch defects while records can prove the correction.
The metrics worth asking any lab for are the ones behind the headline number, not the headline itself.
| Metric | What it tells you | Where it comes from |
|---|---|---|
| First-run pass rate, by failure category | Whether the bench catches faults or buries them | Internal test log, per production run |
| Retest loops per style, before submission | How much schedule the lab is really costing you | Corrective-action record, closed items only |
| Corrective-action closure time | Whether the fix loop actually closes | Corrective-action timestamps, open vs closed |
| Pre-submission rejection rate at the notified body | Whether the in-house “pass” means anything | The body’s own submission feedback |
A headline failure rate without the category breakdown hides more than it shows.
📈 ROI Check: Two figures set the budget, and both come off approved records. Recall exposure avoided is the screened first-run failure count times annual volume times average field-failure cost. Days saved is the external lab queue minus the in-house retest. Use approved numbers only; if the first-run data is not approved, say so instead of quoting it.
Better document-to-sample consistency
Drawings, bills of materials, labels and test records stay aligned before formal submission. A clean bench run means little if sample ID, drawing revision and bill of materials disagree. We check the report pack against the physical sample before it reaches a notified body or certification lab.
That reduces submission rejections and customs holds. It does not guarantee universal certification acceptance, but it gives your team a defensible evidence trail when reviewers ask hard questions — the same file discipline that decides whether a private-label program survives a change of valve mid-season.
Challenges and Limitations: Cost, Scope and the Reality Check
What does lab testing and certification actually cost? No credible lab quotes a fixed number before it knows the program. Price depends on appliance family, gas family, standard route, sample count and retest loops. Anyone who quotes flat before asking is guessing.
Three cost centres buyers confuse
Procurement teams blur three separate budgets:
- In-house pre-compliance screening: fixtures, calibration, operator time, sample preparation.
- Third-party or witnessed testing: notified body fees, CSA/ANSI testing, engineering days, witness travel.
- Final certification and maintenance: type approval, annual surveillance, document upkeep.
A factory bench screens the unit. It does not erase the third-party bill.
Where the testing breaks down
A passed pressure test is a snapshot. It proves the unit held that day, not next month. Uncalibrated instruments produce worthless reports, and a gauge past its calibration date turns every reading after it into noise.
Sample origin matters. A unit built for the domestic China market can still miss CE or CSA nuance — the test gas alone differs. Combustion shifts with gas family, altitude, venting and fixture geometry, so a bench-clean unit can spike CO once installed. Paperwork sinks audits just as quietly: a sample ID that disagrees with the bill of materials revision fails a good unit.
Accreditation, approved body status and certification differ
Buyers say “accredited lab” when they mean three things. Accreditation covers a defined scope and is granted to the laboratory. An approved body (Great Britain) or notified body (EU) is appointed by government to carry out conformity assessment for a named regulation — BSI 0086 and Intertek 0359 are examples. Product certification is the legal market approval itself. A lab can hold one and not the others. Ask which, and ask for the scope.
Buyer objection checklist
Put these questions to any supplier before you commit budget:
- What exact standards and markets does this lab scope support?
- Which tests run in-house, and which go outside?
- Are gauges, analysers and leak detectors within calibration?
- How are failed samples quarantined, corrected and re-tested?
- Can the factory prove traceability from part batch to final test record?
Commercial frictions competitors skip
Sample attrition burns budget. Destructive tests consume units. Retests slip schedules by weeks. Batch-to-batch drift forces fresh runs. Not every factory bench is accepted for witness programmes, so an external body may reject it.
⚠️ Critical Warning: A bench-clean unit is not a field-clean unit. Combustion shifts with gas family, altitude and venting, so a passing bench run on the wrong test gas proves nothing about the market you are shipping to.
⚖️ Trade-off: An integrated bench reduces risk and shortens feedback loops. It never removes the need for scope confirmation, budgeting discipline, or external acceptance where the standard requires it.
The Verdict
A credible factory bench rests on scoped procedures, calibrated equipment, competent operators, clean traceability and a corrective-action loop that closes. Carry this verification hierarchy into every supplier review:
- Market and standard fit: does the bench’s scope match your destination route — (EU) 2016/426, ANSI/CSA, or GB?
- Equipment and calibration fit: are gauges, flowmeters, leak detectors and analysers sized to the test and current on calibration?
- SOP and operator discipline: does the bench run the same sequence every time?
- Failure-log and corrective-action discipline: do defects get logged as symptom, root cause, action and re-test?
- Document-to-sample consistency: do sample ID, bill of materials and drawing revision agree before submission?
When a supplier demonstrates real leakage, pressure and combustion controls on site, audit confidence and launch predictability improve together. Those controls shorten feedback loops and keep unapproved failures away from certification and the field.
Before you commit budget, put the same questions to your own supply base that we put to ours. A bench that cannot answer them on the spot is telling you something. Engineering and procurement teams can request a design review or a full documentation package through our contact page and we will walk the lab line against your specification.
Disclosure: Gulfstone is a manufacturer, not a disinterested third party. Every technical claim above rests on documented bench practice and approved internal records. Where a figure is pending approval, we say so rather than publish an unverified rate, and no kickbacks are accepted from notified bodies, calibration houses or third-party labs.
People Also Ask About Gas Appliance Testing Laboratories
1. What does gas appliance lab testing and certification cost?
No credible gas appliance testing laboratory quotes a fixed price before it knows the program. Factory-level testing cost depends on the appliance family, the gas family, the standard route, the sample count, and how many retest loops the unit needs. Budget three separate lines — in-house pre-compliance screening, third-party or witnessed testing, and final certification with its annual maintenance — and ask for them itemised separately, because a single blended number hides where the money actually goes.
2. What is the difference between testing, calibration, accreditation and certification?
Testing runs a product through a defined procedure and records the result. Calibration proves an instrument still reads true against a traceable reference, normally to ISO/IEC 17025. Accreditation is formal recognition that a laboratory can run a defined scope of tests. Certification is the legal market approval, issued only by a body appointed to grant it. A factory lab can do the first two. It cannot do the last.
3. Which standard applies to my gas appliance?
It depends on the appliance family and the destination market, not the factory. Europe runs on Regulation (EU) 2016/426, with product standards such as EN 30-1-1 for cooking appliances, EN 26 for instantaneous water heaters and EN 89 for storage water heaters. North America uses the ANSI Z21 / CSA 2.x series. China uses GB 16410, GB 6932 and GB 25034 by family. Confirm the exact standard and its edition before tooling, because a late change costs a retest cycle.
4. Does an in-house lab report clear my shipment?
No. An in-house report proves the unit is ready for submission. The certificate that clears customs and puts the CE mark or a North American listing on the product is issued by an accredited third party, a notified or approved body, or a certification body for the relevant standard. Treat the in-house report as evidence of readiness, never as the approval itself.
5. What does the notified body need from us?
Access to the type-examination report, the design documentation, the production line and the facilities. Surveillance runs at least annually and may be reduced in scope if your quality system is accepted. Serial production must stay identical to the approved type. Incomplete traceability — a sample ID that disagrees with the bill of materials or drawing revision — is the most common reason a technically sound unit gets held up.
Forward
Founder & CEO, GulfstoneGas appliance manufacturing and certification
Most of what decides a gas appliance is settled before anything is built — on the drawing, at the cut-out, in the tolerance someone chose for the gas path. I have spent my working life on the manufacturing side of that decision, and this is where I write down what it has taught me.
Nothing here is written from a sales desk. Every note comes off the floor: a batch held until a reason was found, a fitting that failed in transit, an approval path that only made sense once the destination market was fixed. If you read these first, the opening conversation starts at the standard rather than at the beginning.
- Gas water heater engineering
- Design for manufacturing
- Certification path selection
- Private-label tooling
- Off-grid and outdoor water heating
- RV Water Heater Manufacturing Process: Gulfstone’s 12-Stage Line SOPSep 30, 2026
- Downsides of Subcontracting: Hidden Sub-Tier Audit ChecklistSep 29, 2026
- Vet an RV Appliance Manufacturer in China: A Five-Gate AuditSep 28, 2026
- OFHC Copper Heat Exchanger: Engineer More Efficient SystemsSep 21, 2026
- RV Water Heater BTU Sizing: Match Power to Real Water DemandSep 16, 2026
- Proportional Gas Valve RV: Unlock Steady Heat and ControlSep 12, 2026
Two decades on the manufacturing side of gas appliances, from the drawing to the shipping container.
Leads Gulfstone's design-for-manufacturing reviews and the certification path selected for each destination market.
Works directly with OEM and private-label buyers on tooling, tolerances and the approval file.